Neodymium magnets – most powerful on the market

Need strong magnetic field? We offer wide selection of various shapes and sizes. Best choice for domestic applications, garage and industrial tasks. See products with fast shipping.

check magnet catalog

Magnet fishing: strong F200/F400 sets

Begin your hobby related to seabed exploration! Our double-handle grips (F200, F400) provide grip certainty and immense power. Stainless steel construction and strong lines are reliable in challenging water conditions.

choose your set

Reliable threaded grips

Professional solutions for fixing without drilling. Threaded mounts (external or internal) provide instant organization of work on production halls. They are indispensable installing lamps, sensors and banners.

check technical specs

📦 Fast shipping: buy by 14:00, package goes out today!

Przejdź do treści
Dhit sp. z o.o.

How are neodymium magnets made and selected?

Dimensions, grade, coating and operating conditions — a guide before you buy

A neodymium magnet is made from an alloy of neodymium, iron and boron (NdFeB). Whether it suits your project depends on its dimensions, magnetisation and operating conditions. Below you will find a selection checklist, a short manufacturing overview and expandable tables for readers who need more detail.

What should you check before buying?

Start with operating conditions, not the highest number after N. Compare specific products with the dimensions and mounting arrangement your project needs.

Dimensions and shape
Specify the mounting space, diameter or length, width and thickness. Check tolerances and whether a hole is needed. Read the details
Material grade
N38 or N52 describes the material, not a lifting capacity in kilograms. Grade alone is not enough to select a product. Read the details
Operating temperature
Consider the temperature of the magnet itself, including during bonding or equipment operation. Do not select it using the Curie point. Read the details
Moisture and coating
State whether the magnet will work in a dry interior, outdoors or in contact with liquid. Its coating and any enclosure must suit those conditions. Read the details
Magnetisation direction
Specify which surfaces need the poles. Two magnets with identical dimensions may need a different arrangement in a device. Read the details
Actual loading conditions
Check whether the part will be pulled away or slid along a surface. The base material, gap and force direction affect the result. Read the details

For DHIT N50, N52 and N54 models, the maximum operating temperature is 60°C. Curie temperature is not the permitted operating temperature. Check the product page for other versions.

Compare magnets in the shop Open the magnet calculator

How is a magnet made? Four stages

  1. Preparing the material. An alloy of neodymium, iron and boron is processed into a fine powder.
  2. Pressing and sintering. A magnetic field aligns the particles during pressing. Sintering densifies the material.
  3. Sizing and coating. Machining produces the required shape. A coating protects the corrosion-prone material.
  4. Magnetising. An external field magnetises the finished part. The required pole arrangement must be specified beforehand.

We import neodymium magnets directly from a factory in China. In Ożarów Mazowiecki, Poland, we manufacture magnetic separators, rods and beams. This description of the NdFeB process does not mean that we sinter magnets in Poland.

What should your enquiry include?

If a stock product does not fit your project, send a description of the application. To assess a custom version or a possible alternative, prepare:

  • A drawing with dimensions and tolerances, or an existing product reference.
  • The required quantity and whether this is a prototype or a repeat order.
  • Temperature, moisture and contact with liquids or chemicals.
  • The mounting method, base material, gap and load direction.
  • The required pole arrangement, coating and preferred delivery date.

Not sure which grade or coating you need? Describe the operating conditions instead of guessing. Feasibility, tolerances and lead time must be confirmed for each enquiry.

Contact us about your project Information for businesses

Technical details and tables

Expand only the topic you need. The content is also available without JavaScript; on a phone, wide tables can be scrolled horizontally.

Full list of topics
Material, safety and magnetic terminology

Safety and operation principles

Critical conditions excluding the use of standard NdFeB magnets without specialized shielding:

  • In acidic, alkaline, organic or dissolving environments (unless you hermetically isolate the magnet from the environment), or radioactive rays
  • In water or oil (unless you isolate the magnet from the environment or are prepared for the magnet to lose its magnetic properties in a short time)
  • In an electrically conductive fluid - electrolyte containing water
  • In an atmosphere containing hydrogen
welding with a magnet

Material specification

Neodymium magnet (NdFeB) is a sintered rare-earth metal, currently the strongest permanent magnet available. It is characterized by an anisotropic tetragonal crystal structure of Nd2Fe14B. Compared to ferrites, it offers approx. 10 times higher energy density (BH)max, allowing for significant device miniaturization.

Due to the high iron content (approx. 64-68%) and neodymium, the neodymium-rich phase at the grain boundaries is highly reactive. This requires the use of barrier coatings (Ni-Cu-Ni, Epoxy, Parylene). An unprotected magnet oxidizes, forming hydroxides, leading to structural disintegration.

The material is brittle (ceramic-like). Machining is only possible with diamond tools before magnetization. Mechanical shocks should be avoided, as they can lead to micro-cracks (chipping).

Neodymium (Nd, atomic number 60) is a key component of the alloy. It is estimated that approx. 20-30% of neodymium in magnets is actually Praseodymium (Pr). Due to chemical similarity, a Pr-Nd alloy is used, which does not negatively affect the magnet's properties. In high-temperature magnets (UH, EH), part of the neodymium is replaced by Dysprosium (Dy) or Terbium (Tb).

  • patent discovery year: 1984 (Sagawa / Croat)
  • Nd atomic number: 60
  • atomic mass: 144.24 u
  • electronegativity (Pauling): 1.14
  • valence: +3
  • phase melting temp.: 1024°C
  • boiling point: 3074°C
  • stable isotopes: 5 (142, 143, 145, 146, 148)
  • configuration: [Xe] 4f4 6s2

Permanent magnet definition

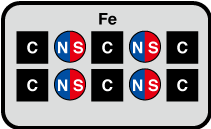
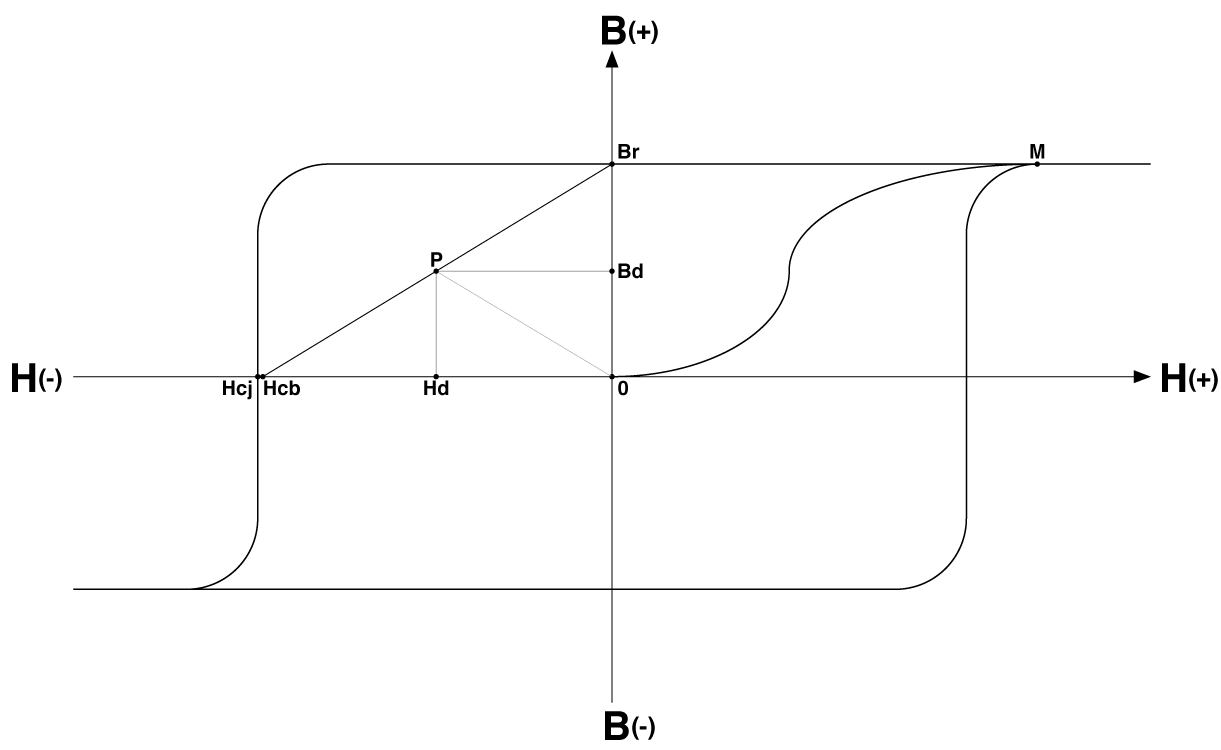
A permanent magnet is a material with a wide magnetic hysteresis loop, capable of maintaining magnetization after the external magnetizing field is removed. A key parameter is high coercivity (Hcj), preventing spontaneous demagnetization.

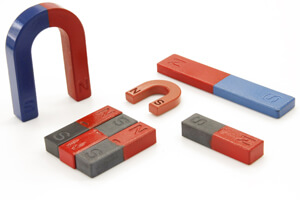
Permanent magnet example

Demagnetization and Curie point

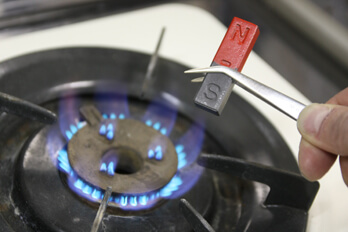
Loss of magnetic properties occurs under the influence of temperature (thermal agitation of domains) or an opposing magnetic field. The Curie point (Tc) is the temperature at which the material loses ferromagnetic properties and becomes paramagnetic (for NdFeB approx. 310-350°C).

reduced magnetization example
Pierre Curie

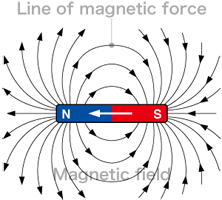
Nature of magnetism

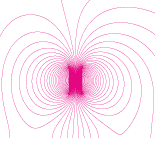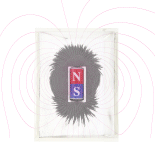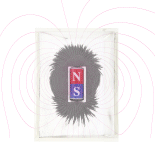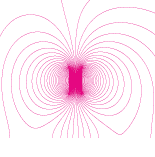
A physical phenomenon resulting from the angular momentum (spin) of electrons and their orbital motion. In NdFeB magnets, the exchange coupling between iron atoms and rare earths plays a key role.

Magnetic force illustration
magnetic flux density

Evaluation methodology (BH curve)

Professional magnet evaluation is performed using a hysteresigraph (BH analyzer). It determines four key points in the 2nd quadrant of the coordinate system: Br (remanence), HcB (induction coercivity), HcJ (polarization coercivity), and (BH)max.

magnet force diagram

Flux density (B)

Magnetic induction measured on the magnet surface (surface gauss). This value depends not only on the magnet grade (Br) but also on its geometry (permeance coefficient - Pc).

Magnetic flux density

Coercivity (Hcb / Hcj)

Resistance to demagnetization. Hcb (normal coercivity) defines the point of zero induction, Hcj (intrinsic coercivity) defines the point of zero polarization - this is a key parameter for temperature resistance.

Maximum energy product (BH)max

The maximum amount of magnetic energy stored per unit volume of material. This value (in MGOe) roughly corresponds to the magnet grade number (e.g., N52 has approx. 52 MGOe).

Pull force (attraction)

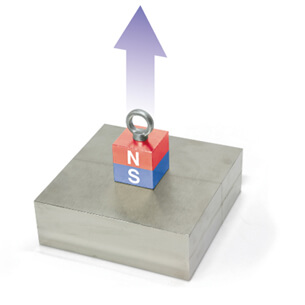
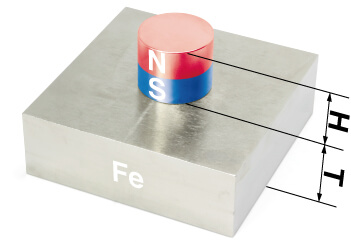
The perpendicular force required to detach a magnet from a low-carbon ferromagnet, with zero air gap. Laboratory values may differ from real ones due to surface roughness, steel composition, or force application angle.

pull force

Shear force (sliding load)

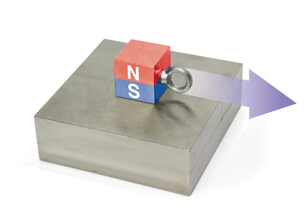
Force acting parallel to the contact surface. It depends directly on the friction coefficient (µ) between the magnet coating and the substrate. For Ni-Cu-Ni coating, it is usually 15-20% of the vertical pull force. Using rubber increases this coefficient.

magnet sliding friction
Force measurement and magnetisation direction

Measurement procedures

Measurement standards in the DHIT laboratory:

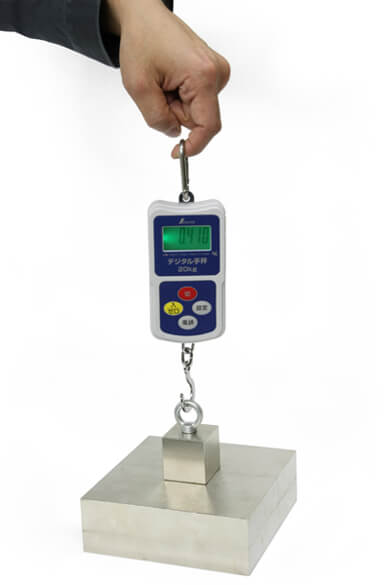
  1. Pull-force test (perpendicular)

    Perpendicular detachment at a speed of 10mm/min from a steel plate (St37) with a thickness of min. 10mm, ground.

    pull force
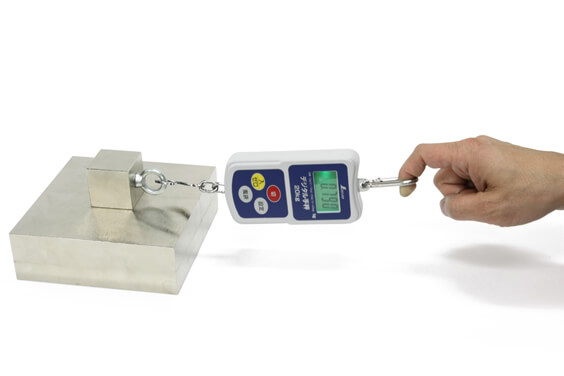
  2. Shear-force test (sliding)

    Parallel sliding. The result is strongly dependent on the coating. For Ni, it is approx. 0.15-0.20 of the vertical force.

    pull force

Measurement boundary conditions

Variables affecting the measurement result:

  • Plate thickness: steel that is too thin becomes magnetically saturated, lowering the result.
  • Positioning: central application of force.
  • Working area: no plate edges in the immediate vicinity.
  • Steel grade: preferred pure armco iron or low-carbon steel.
  • Surface roughness (Ra).
  • Air gap: even 0.1mm drastically reduces the force.
Ambient conditions cube
Ambient conditions pipe
Ambient conditions cylinder

Anisotropy and magnetization directions

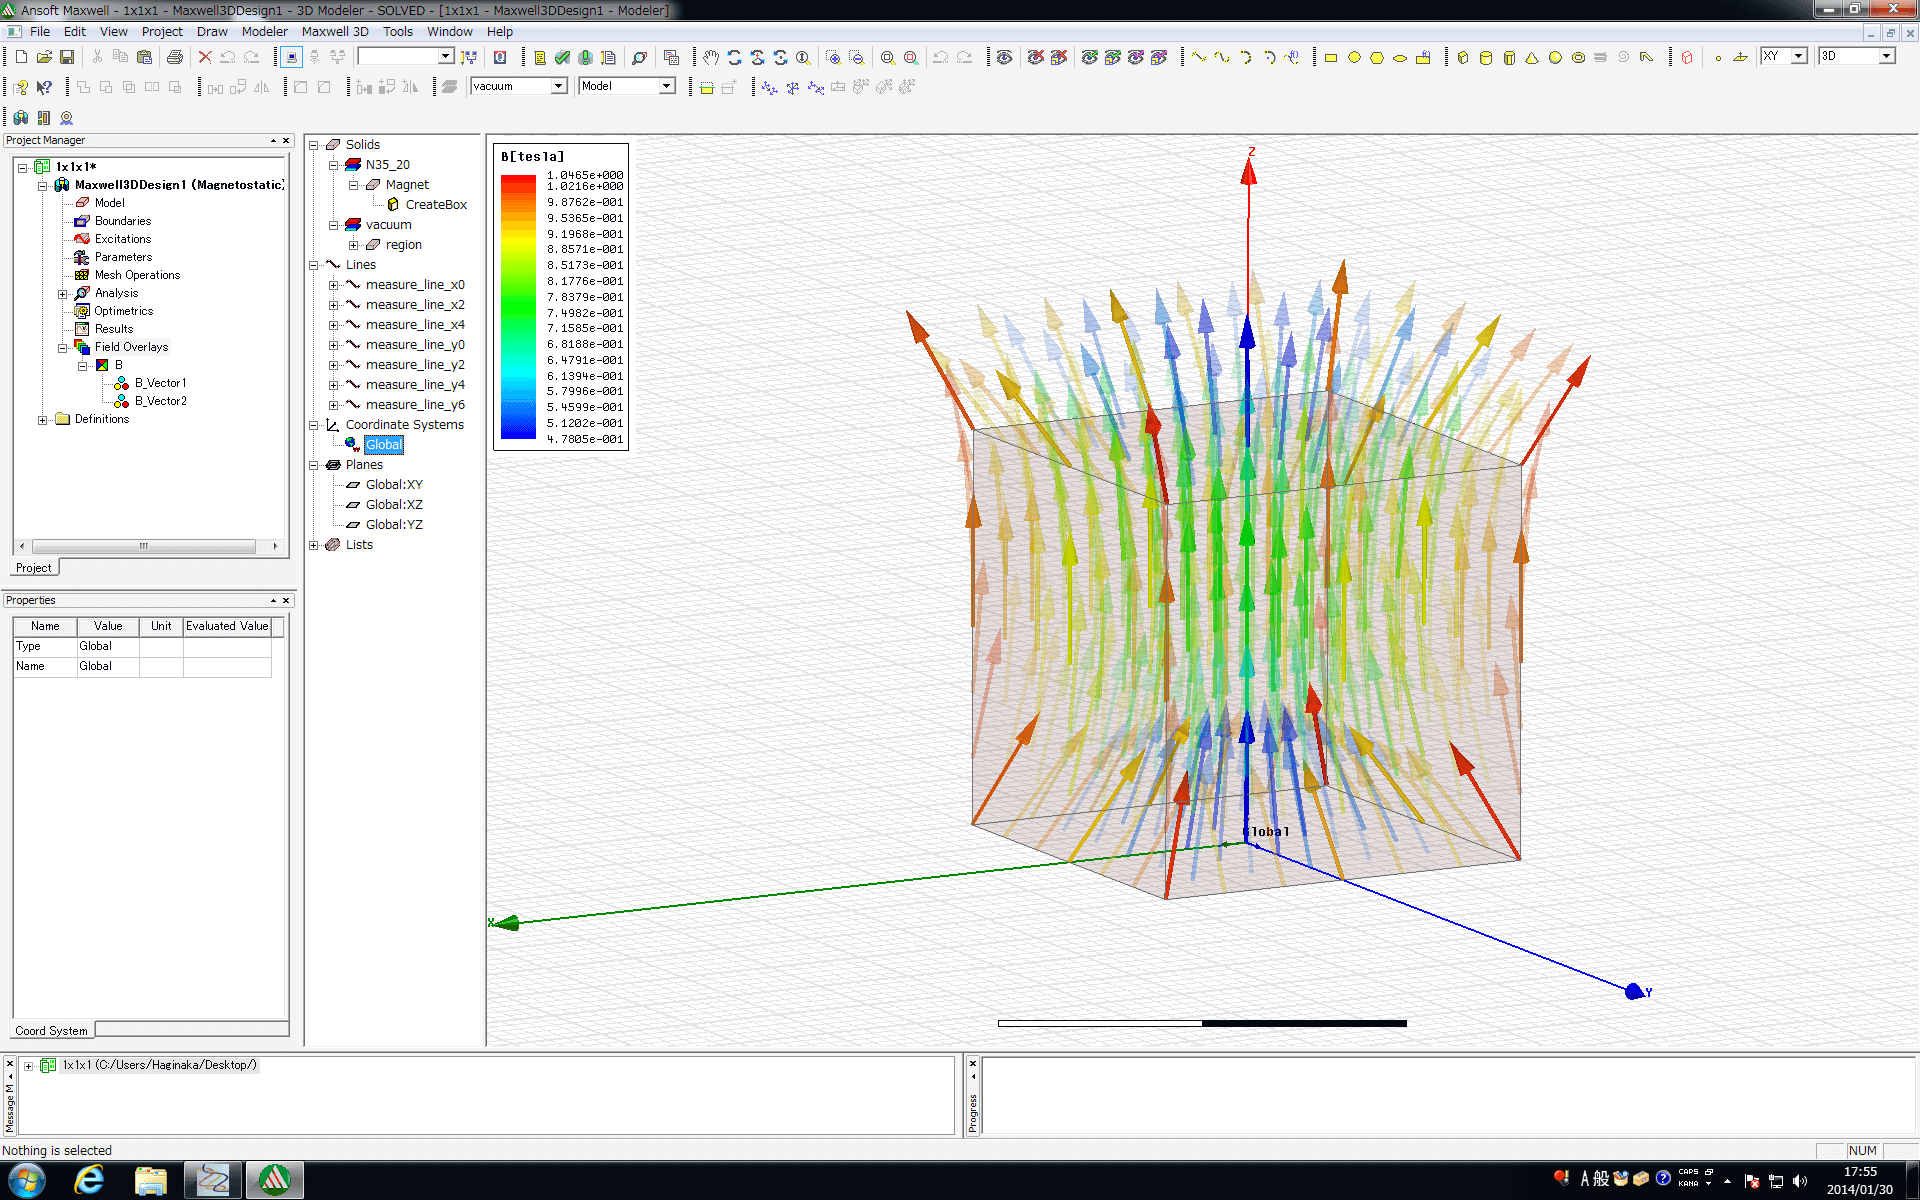
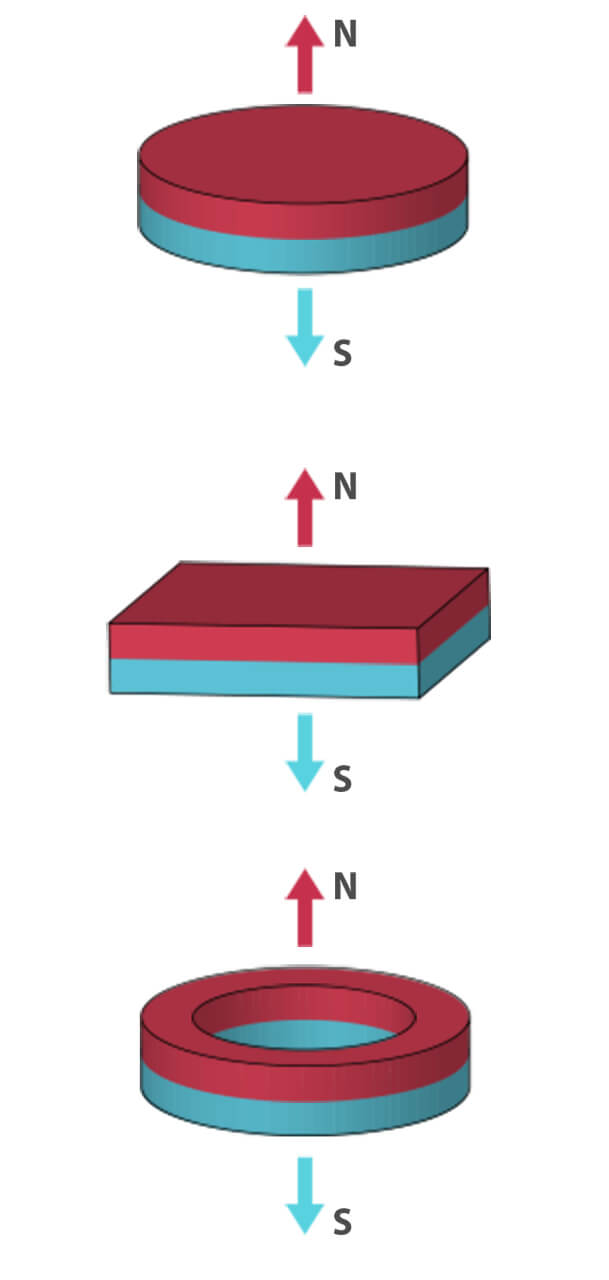
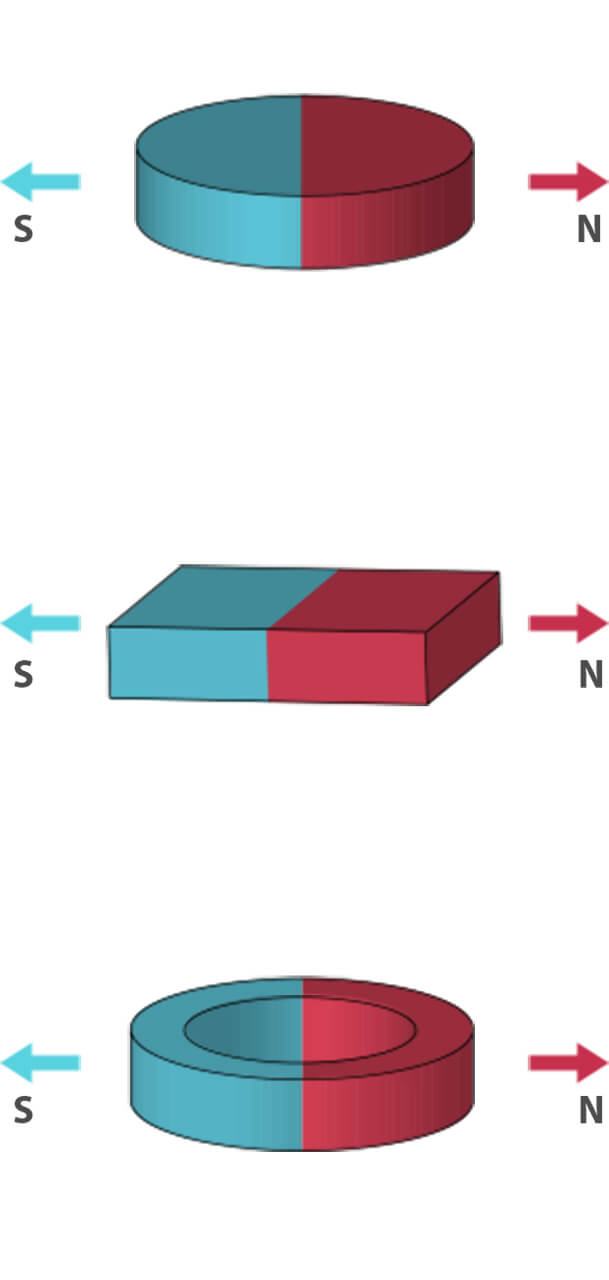
NdFeB sinters are anisotropic materials – the direction of easy magnetization is established during powder pressing in a magnetic field.

Axial

Magnetization vector parallel to the axis of symmetry (height). Most common configuration for cylinders and rings.

axial magnetization

Diametrical

Magnetization vector perpendicular to the axis of symmetry (through the diameter).

diametrical magnetization

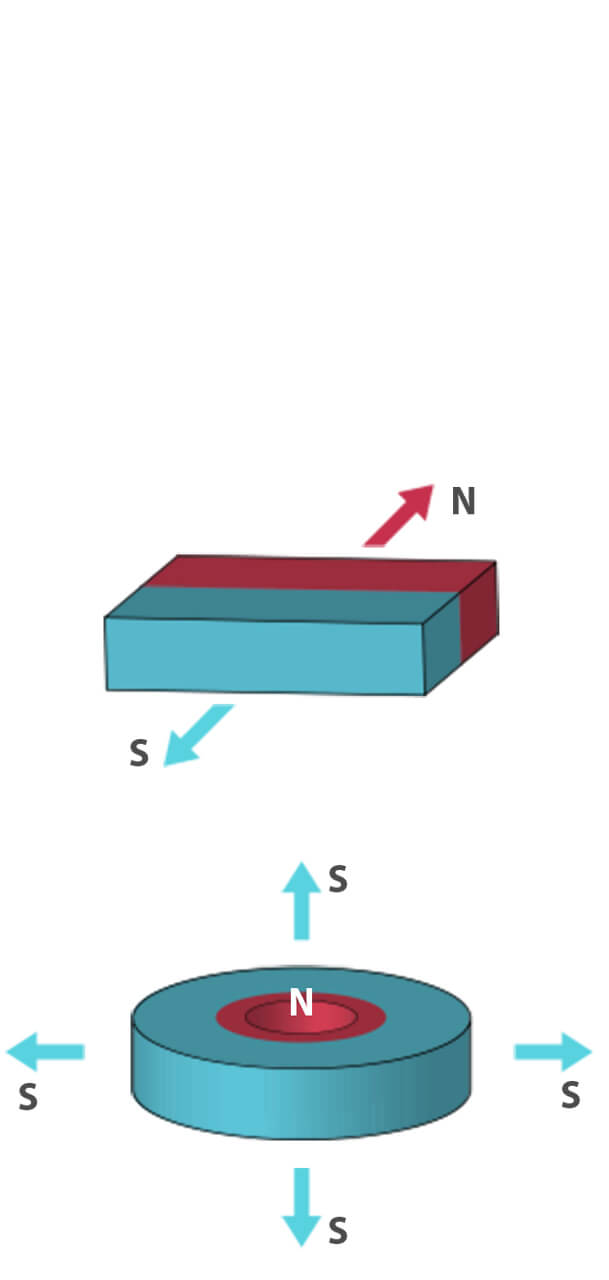
Radial (multipole)

Specialized orientation (requires a separate mold for pressing). Poles distributed on the circumference.

radial magnetization

Magnetic poles are always located on surfaces perpendicular to the orientation direction (easy axis).


Cylindrical magnets

  • axial: poles on flat bases.
  • diametrical: poles on the cylinder curves.
  • radial: multipole on the circumference (for rotors).

Plate magnets (blocks)

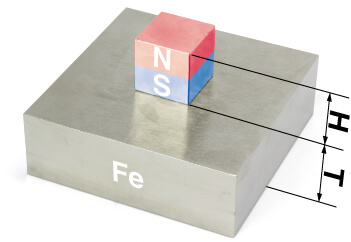
  • through thickness (H): standard.
  • through width (W).
  • through length (L).

Ring magnets

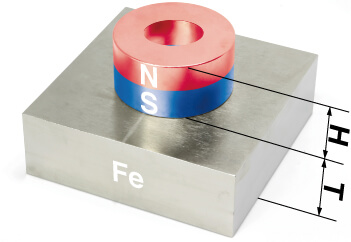
  • axial: standard.
  • diametrical: 2 poles on the circumference.
  • radial: special execution.
Manufacturing, coatings and corrosion

A detailed description of the sintering process

Sintered neodymium magnet production is an advanced powder metallurgy process in which an alloy of neodymium, iron and boron is formed in a strong magnetic field.

  1. Strip casting. The process begins by melting the charge in an induction furnace under a protective argon atmosphere. The molten metal is poured onto a rotating, water-cooled copper roller and solidifies into thin flakes (SC alloy).
  2. Hydrogen decrepitation and jet milling. The material undergoes the HD (Hydrogen Decrepitation) process — hydrogen penetrates the structure and breaks the ingots into fine particles. Jet mills operating in a nitrogen atmosphere then reduce the powder to a grain diameter of about 3 µm.
  3. Pressing and sintering. The powder is pressed in a strong magnetic field, which aligns the domains and gives the material anisotropy — a preferred direction of magnetisation. The “green” compacts go into vacuum furnaces at about 1050°C. Sintering is followed by two-stage annealing at 900°C and 600°C, which relieves internal stress and dissolves unstable phases.
  4. Machining and magnetisation. The sinters are cut to size with precision wire saws, which limits kerf losses of the costly material. After the protective coating is applied, the magnets are activated in pulse magnetisers with a field of around 5 T.

Alternative production methods (special technologies)

In addition to classic sintering, advanced methods are used to obtain specific properties:

1. Hydrogen method HDDR

The process (Hydrogenation, Disproportionation, Desorption, Recombination) takes place at 750-900°C. It allows obtaining powder with a very fine-grained structure and high coercivity. This material is often used for the production of bonded magnets.

2. Bonded Magnets

A mixture of magnetic powder (NdFeB) with a polymer binder (resin, plastic). Produced by injection molding or compression molding. Although they have weaker magnetic parameters than sintered ones, they are characterized by high shape precision without the need for machining, greater corrosion resistance, and flexibility.

3. Mechanical alloying

Milling powder in ball mills, leading to a nanocrystalline structure. After short annealing (approx. 700°C), a material with very high coercivity is obtained.

Surface engineering (coatings)

Due to the low corrosion resistance of the Nd-rich phase, coatings are mandatory. The thickness and type of coating affect dimensional tolerances and environmental resistance.

Ni-Cu-Ni (standard)

  • Features: structure: nickel (base) + copper (elasticity/tightness) + nickel (finish).
  • Color: appearance: silvery gloss.
  • Price: advantages: best price-to-protection ratio.
  • Thickness: thickness: 10-20 µm.

Ni-Cu-Ni-Au (gold)

Decorative and functional coating (conductivity).

  • Layer: top layer: 24k industrial gold (thin layer).
  • Color: application: medical (biocompatibility), electrical contacts.
  • Au Thickness: Au thickness: ~0.05-0.1 µm.
  • Total Thickness: base: requires full Ni-Cu-Ni undercoat.

Ni-Cu-Ni-Cr (chrome)

  • Resistance: advantages: high resistance to abrasion (friction).
  • Color: appearance: cold, bluish gloss.
  • Thickness: thickness: ~15 µm.

Ni-Cu (copper)

Used less frequently as a final layer.

  • Color: application: lower resistance, mainly aesthetic or as a base.
  • Abrasion: disadvantage: copper quickly passivates (darkens).
  • Corrosion: costs: lower than triple layer.
  • Thickness: thickness: ~10 µm.

Epoxy (resin)

Black electrophoretic or spray coating

Ideal for marine and outdoor applications, as long as it is not exposed to impact.

  • Color: resistance: excellent against moisture and salt spray.
  • Corrosion: disadvantage: brittle, prone to mechanical scratches.
  • Resistance: insulation: electrical.
  • Thickness: thickness: 15-30 µm.

Rubber coated

Dedicated to automotive and mounting holders.

  • Color: material: santoprene or synthetic rubber.
  • Impact: function: increases friction (shear force), protects substrate paint.
  • Friction: disadvantage: air gap (rubber thickness 0.5mm) significantly reduces perpendicular force.
  • Thickness: thickness: 0.5 - 1.0 mm.
  • Chemicals: water resistance: very high.
  • Force: impact resistance: absorbs shocks.

Plastic overmolding

Full environmental protection.

  • Color: material: ABS, PP, Nylon.
  • Impact: tightness: complete (hermetic).
  • Friction: durability: very high.
  • Thickness: wall thickness: 1-2 mm.
  • Chemicals: application: clothing industry, toys.
  • Force: force reduction: significant (large gap).

Technical parameters of coatings

Detailed comparative data on corrosion resistance (SST and PCT tests):

material symbol coating thickness (μm) corrosion resistance (salt spray) (Hr) porosity demagnetization rate color PCT (Hr)
Zinc Zn 10-15 >24 <0.1 <0.2% White >16
Colorful zinc Colorful-Zn 10-15 72 <0.1 <0.1% Multicolor >24
Nickel Ni 10-20 4 <0.5 <0.3% Silver >16
Double nickel Divalent-Ni 15-20 24 <0.2 <0.3% Silver >16
Nickel-copper-nickel Ni-Cu-Ni 15-30 >48 <0.1 <0.1% Silver >42
Zinc-nickel alloy Zn-Ni alloy 10-20 >720 <0.1 <0.1% Various colors >72
Third-party epoxy Epoxy 10-50 >300 - - Black >24
Electroless nickel electroless Ni <1 >72 - - Silver >24

Salt chamber test: 37-39°C 5% NaCl PH 6.5-7.0 1.5 ml/Hr
PCT: 120°C, 2atm, 100% RH, 12Hr.

Appearance and characteristics

φ10mm×10mm
Element symbol
Element name
Properties
Usage
3CrZn
3CrZn Trivalent chromium zinc Recently hexavalent chromium has been recognized as an environmentally damaging substance and replaced by trivalent chromium Electronic parts, industrial tool parts
Ag
Ag Silver Silver has the best electrical conductivity of all metals, low contact resistance, and good solderability, but is easy to discolor. Electronic parts, Connectors, Dishes, Accessories
Au
Au Gold Gold has good corrosion and oxidation resistance and low electrical resistance. Electronic parts, Electrical parts, Decorations, Accessories
Cr
Cr Chrome Chrome has good abrasion and oxidation resistance and does not lose its shine in the atmosphere. Exterior parts, Medical supplies, Audiovisual equipment, Accessories
Cu
Cu Copper Copper discolors easily, so it is used as a base. Used to fill dents and add shine. Cast products, ABS resin base
CuZn
CuZn Bronze Brass materials change color easily and are usually used as an undercoat. Brass materials are often used in ancient ornaments. Ancient colorful ornaments
Ni
Ni Nickel Nickel is chemically stable and has good anti-corrosion properties. It can be used for many different purposes and is used as a base for gold plating, chrome plating, etc. May cause skin irritation. Electronic parts, Connectors, Base plating, Accessories
NiBlack
NiBlack Black nickel Black nickel is an alloy coating made of nickel, zinc, and sulfur. The color may vary depending on the type of plating used as an undercoat. Decorations, Accessories
Sn
Sn Tin Tin has excellent anti-corrosion properties and does not oxidize easily. It does not lose its shine easily and can be safely used in food products. Food dishes, Cans, Tin items, Decorations, Accessories
Rh
Rh Rhodium Rhodium has excellent anti-corrosion properties and does not oxidize easily. It does not lose its shine easily and can be safely used in food products. Electronic parts, Electrical parts, Audio parts, Decorations, Accessories
Chrom cynk leczniczy
- Untreated No surface treatment coating. Rust will easily develop on neodymium magnets.
Nylon
- Nylon Made without organic solvents and used in food processors and medical devices. Passed the food hygiene act. Toys, Small items
MF305
- Polyamide MF305 High impact strength, bending resistance, and possibility of use at high temperature. Electronic parts, Small items, For bending after painting
- - Epoxy MF304 High resin hardness / Flame retardancy adjustment: UL94 / V-0 Certified
- - Epoxy MF303 High resin hardness / Easy to polish

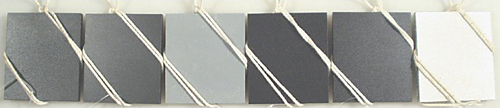
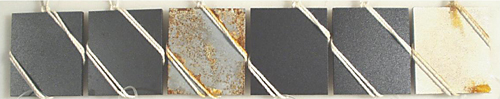
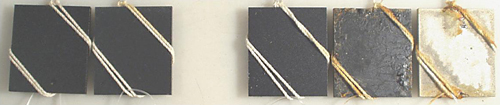
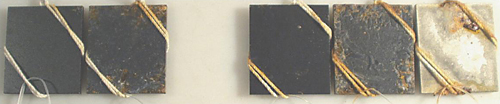
Rust resistance test Ni / Zu / Epoxy resin

  Dhit Company [S] Other companies Dhit Company [T] Dhit
Duration HDC coating, Epoxy resin, MF304 Normal epoxy resin Anti-corrosion Zn primer for Zn car HDC, Epoxy resin coating, MF305 epoxy resin NiCuNi, 3 layers, nickel
Before starting test
magnet salt test
After 72 hrs
72h
After 312 hrs
312h
After 504 hrs
504h

Salt chamber test: 37-39 °C 5% NaCl PH 6.5-7.0 1.5 ml/Hr
PCT: 120°C, 2atm, 100% RH, 12Hr.

Temperature, properties and engineering tables

These are reference data about materials and technologies, not confirmation that every grade, dimension or tolerance is available in the shop. Check the product page or confirm the parameters and tolerances of the particular version in your enquiry.

Thermal stability and magnetic losses

Depending on temperature, we distinguish three different types of losses:

  • reversible (can be undone)
  • irreversible (cannot be undone)
  • constant

Reversible temperature loss

  • temperature area: slightly above maximum operating temperature,
  • temperature area: slightly above maximum operating temperature
  • magnet is less magnetic if it is hot
  • it does not matter how often the magnet is heated and cooled

Irreversible loss

  • temperature area: significantly above maximum operating temperature
  • magnet is permanently weakened, even after cooling
  • repeated heating at the same temperature does not strengthen irreversible losses
  • magnetization of an irreversibly weakened magnet by a sufficiently strong external magnetic field can restore its original strength

Constant loss of magnetic properties

due to high temperature, the structure of neodymium magnets changes - magnetization is no longer possible

Engineering tables (advanced data)

Mechanical properties
Young's Modulus (E) 160 GPa
Poisson's Ratio (ν) 0.24 -
Compressive strength 1000 - 1100 MPa
Tensile strength 80 MPa
Vickers Hardness (Hv) 560 - 600 Hv
Density 7.4 - 7.6 g/cm³
Thermal properties
Specific heat 460 J/(kg·K)
Thermal conductivity 6 - 9 W/(m·K)
Expansion coefficient (parallel) 5.2 x 10⁻⁶ /°C
Expansion coefficient (perpendicular) -0.8 x 10⁻⁶ /°C
Standard geometric tolerances (ISO)
Dimension (L, W, H) ±0.05 mm (standard) / ±0.02 mm (precision)
Diameter (D) ±0.05 mm
Flatness < 0.05 mm
Parallelism < 0.05 mm
Perpendicularity < 1°
Magnetic unit converter
1 Tesla (T) 10,000 Gauss (G)
1 kA/m 12.57 Oersted (Oe)
1 MGOe 7.96 kJ/m³

Maximum production dimensions for NdFeB magnets

shape sketch parameters
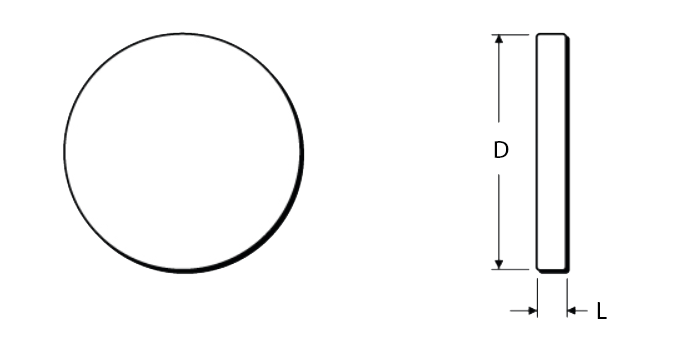
cylindrical magnet
cylindrical magnet
dimension
D(mm) L(mm) magnetization direction
all grades 1.0 ~ 250 mm ≤ 80 mm axial or radial
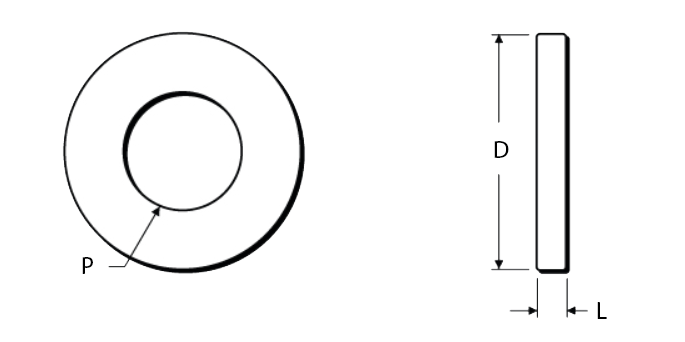
ring magnet
ring magnet
dimension
D(mm) P(mm) L(mm) magnetization direction
all grades 2.5 ~ 250 mm 0.8 ~ 230 mm ≤ 80 mm ≤ 80 mm
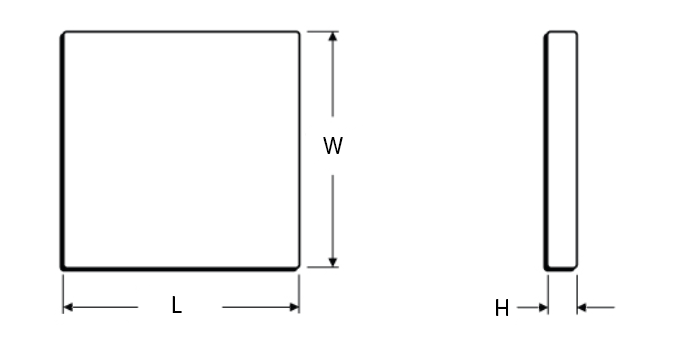
plate magnet
plate magnet
dimension
L(mm) W(mm) H(mm) magnetization direction
all grades ≤ 200 mm ≤ 100 mm ≤ 80 mm ≤ 80 mm
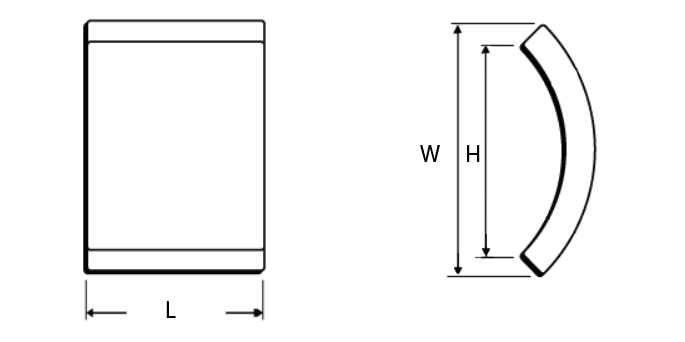
segment
segment
dimension
H(mm) W(mm) L(mm) magnetization direction
all grades ≤ 70 mm ≤ 100 mm ≤ 200 mm ≤ 80 mm

Magnetic properties of sintered neodymium magnets NdFeB

material type remanence coercivity actual intrinsic force energy density operating temperature
Br(kGs) Br(mT) (BH)max(MGOe) (BH)max(kJ/m³)
Min. - Max. Min. - Max. bHc(kOe) bHc(kA/m) iHc(kOe) iHc(kA/m) Min. - Max. Min. - Max.
N3010.8-11.21080-11209.8-10.5780-836≥12≥95528-30223-239≤ 80°C
N3311.4-11.71140-117010.3-11820-876≥12≥95531-33247-263≤ 80°C
N3511.7-12.11170-121010.8-11.5860-915≥12≥95533-35263-279≤ 80°C
N3812.2-12.61220-126010.8-11.5860-915≥12≥95536-38287-303≤ 80°C
N4012.6-12.91260-129010.5-12.0860-955≥12≥95538-40303-318≤ 80°C
N4212.9-13.21290-132010.8-12.0860-955≥12≥95540-42318-334≤ 80°C
N4513.2-13.71320-137010.8-12.5860-995≥12≥95543-45342-358≤ 80°C
N4813.7-14.21370-142010.8-12.5860-995≥12≥95545-48358-382≤ 80°C
N5014-14.61400-146010.8-12.5860-995≥12≥95547-51374-406≤ 60°C
N5214.2-14.71420-147010.8-12.5860-995≥12≥95548-53380-422≤ 60°C
N5414.5-15.11450-151010.8-12.5860-995≥12≥87651-55406-438≤ 60°C
N30M10.8-11.21080-11209.8-10.5780-836≥14≥111428-30223-239≤100°C
N33M11.4-11.71140-117010.3-11820-876≥14≥111431-33247-263≤100°C
N35M11.7-12.11170-121010.8-11.5860-915≥14≥111433-35263-279≤100°C
N38M12.2-12.61120-126010.8-11.5860-915≥14≥111436-38287-303≤100°C
N40M12.6-12.91260-129010.8-12860-955≥14≥111438-40303-318≤100°C
N42M12.9-13.21290-132010.8-12.5860-995≥14≥111440-42318-334≤100°C
N45M13.2-13.71320-137010.8-13860-1035≥14≥111443-45342-358≤100°C
N48M13.7-14.21370-142010.8-12.5860-995≥14≥111445-48358-382≤100°C
N50M14-14.61400-146010.8-12.5860-995≥14≥111447-51374-406≤100°C
N27H10.2-10.61020-10609.5-10.1756-804≥17≥135325-27199-215≤120°C
N30H10.8-11.21080-112010.1-10.6804-844≥17≥135328-30223-239≤120°C
N33H11.4-11.71140-117010.3-11820-876≥17≥135331-33247-263≤120°C
N35H11.7-12.11170-121010.8-11.5860-915≥17≥135333-35263-279≤120°C
N38H12.2-12.61120-126010.8-11.5860-915≥17≥135336-38287-303≤120°C
N40H12.6-12.91260-129010.8-12860-955≥17≥135338-40303-318≤120°C
N42H12.9-13.21290-132010.8-12860-955≥17≥135340-42318-334≤120°C
N44H13.2-13.61320-136010.8-13860-1035≥17≥135342-44334-350≤120°C
N48H13.7-14.21370-142010.8-12.5860-995≥17≥135345-48358-382≤120°C
N27SH10.2-10.61020-10609.5-10.1756-804≥20≥159225-27199-215≤150°C
N30SH10.8-11.21080-112010.1-10.6804-844≥20≥159228-30223-239≤150°C
N33SH11.4-11.71140-117010.3-11820-876≥20≥159231-33247-263≤150°C
N35SH11.7-12.11170-121010.8-11.5860-915≥20≥159233-35263-279≤150°C
N38SH12.2-12.61120-126010.8-11.5860-915≥20≥159236-38287-303≤150°C
N40SH12.6-12.91260-129010.8-12.0860-955≥20≥159238-40303-318≤150°C
N42SH12.9-13.21290-132010.8-12860-955≥20≥159240-42318-334≤150°C
N45SH13.2-13.71320-137010.8-12.5860-955≥20≥159243-45342-358≤150°C
N25UH9.8-10.2980-10209.2-9.6732-764≥25≥199023-25183-199≤180°C
N28UH10.4-10.81040-10809.8-10.2780-812≥25≥199026-28207-233≤180°C
N30UH10.8-11.21080-112010.1-10.6804-844≥25≥199028-30223-239≤180°C
N33UH11.4-11.71140-117010.3-11820-876≥25≥199031-33247-263≤180°C
N35UH11.7-12.11170-121010.8-11.5860-915≥25≥199033-35263-279≤180°C
N38UH12.2-12.61120-126010.8-11.5860-915≥25≥199036-38287-303≤180°C
N40UH12.6-12.91260-129010.5-12.0860-955≥25≥199038-40303-318≤180°C
N25EH9.8-10.2980-10209.2-9.6732-764≥30≥238823-25183-199≤200°C
N28EH10.4-10.81040-10809.8-10.2780-812≥30≥238826-28207-223≤200°C
N30EH10.8-11.21080-112010.1-10.6804-844≥30≥238828-30223-239≤200°C
N33EH11.4-11.71140-117010.3-11820-876≥30≥238831-33247-263≤200°C
N35EH11.7-12.11170-121010.8-11.5860-915≥30≥238833-35263-279≤200°C
N38EH12.2-12.51120-1250≥11.3≥899≥30≥238836-39287-310≤200°C
N40EH12.5-12.81250-1280≥11.6≥923≥30≥238838-41302-326≤200°C
N42EH12.8-13.21280-1320≥11.7≥931≥30≥238840-43318-342≤200°C
N28AH10.4-10.81040-1080≥9.9≥787≥33≥262426-29207-231≤230°C
N30AH10.8-11.31080-1130≥10.3≥819≥33≥262428-31223-247≤230°C
N33AH11.3-11.71130-1170≥10.6≥843≥33≥262431-34247-271≤230°C
N35AH11.7-12.21170-1120≥11.0≥876≥33≥262433-36263-287≤230°C
N38AH12.2-12.51120-1250≥11.3≥899≥33≥262436-39287-310≤230°C
N40AH12.5-12.81250-1280≥11.6≥923≥33≥262438-41302-326≤230°C

* The above-mentioned data regarding magnetic and physical properties are given at room temperature (20°C). The maximum operating temperature of the magnet may change due to the length-to-diameter ratio, coating thickness, and other environmental factors. Additional grades are available. Please contact us for information.

Temperature properties of neodymium magnets

For DHIT N50, N52 and N54 models, the maximum operating temperature is 60°C. Curie temperature is not the permitted operating temperature. Check the product page for other versions.

The table below contains information about the maximum operating temperature (Maximum Operating Temperature) and Curie temperature (Curie Temperature) for individual grades ("N Grade"). Knowledge of these parameters is particularly important when selecting a magnet for applications in elevated temperature conditions.

magnet type/grade maximum operating temperature Curie temperature
N30–N4880°C / 176°F310°C / 590°F
N50 / N52 / N54 (DHIT)60°C / 140°F—
NM100°C / 212°F340°C / 644°F
NH120°C / 248°F340°C / 644°F
NSH150°C / 302°F340°C / 644°F
NUH180°C / 356°F350°C / 662°F
NEH200°C / 392°F350°C / 662°F
NAH230°C / 446°F350°C / 662°F

Influence of Heavy Rare Earth Elements (Dy/Tb/Ho)

The table below illustrates the classification of sintered materials based on production technology. The blue area (HREE FREE) indicates magnets produced without the use of heavy rare earth elements. The yellow area requires doping with Dysprosium (Dy) or Terbium (Tb) to obtain high coercivity.

HREE FREE (Without heavy elements)
With heavy elements (Dy/Tb/Ho)
Br (kGs) Max Temp
N grades
check product limits
100°C
(M)
120°C
(H)
150°C
(SH)
180°C
(UH)
200°C
(EH)
220°C
(AH)
250°C
(TH)
14.8 - 15.2 60N 60M 60H 60SH - - - -
14.6 - 14.9 58N 58M 58H 58SH - - - -
14.3 - 14.6 55N 55M 55H 55SH 54UH - - -
14.0 - 14.3 52N 52M 52H 52SH 52UH 52EH - -
13.7 - 14.0 50N 50M 50H 50SH 50UH 50EH - -
13.2 - 13.6 48N 48M 48H 48SH 48UH 48EH - -
12.8 - 13.2 45N 45M 45H 45SH 45UH 45EH 45AH -
12.5 - 12.8 42N 42M 42H 42SH 42UH 42EH 42AH -
12.2 - 12.5 40N 40M 40H 40SH 40UH 40EH 40AH 40TH
11.8 - 12.2 38N 38M 38H 38SH 38UH 38EH 38AH 38TH
11.3 - 11.7 35N 35M 35H 35SH 35UH 35EH 35AH 35TH
Hcj (kOe) → 12 14 17 20 25 30 35 40
Dhit sp. z o.o.

e-mail: bok@dhit.pl

tel: +48 888 99 98 98